XM220 Pulse
Descriere
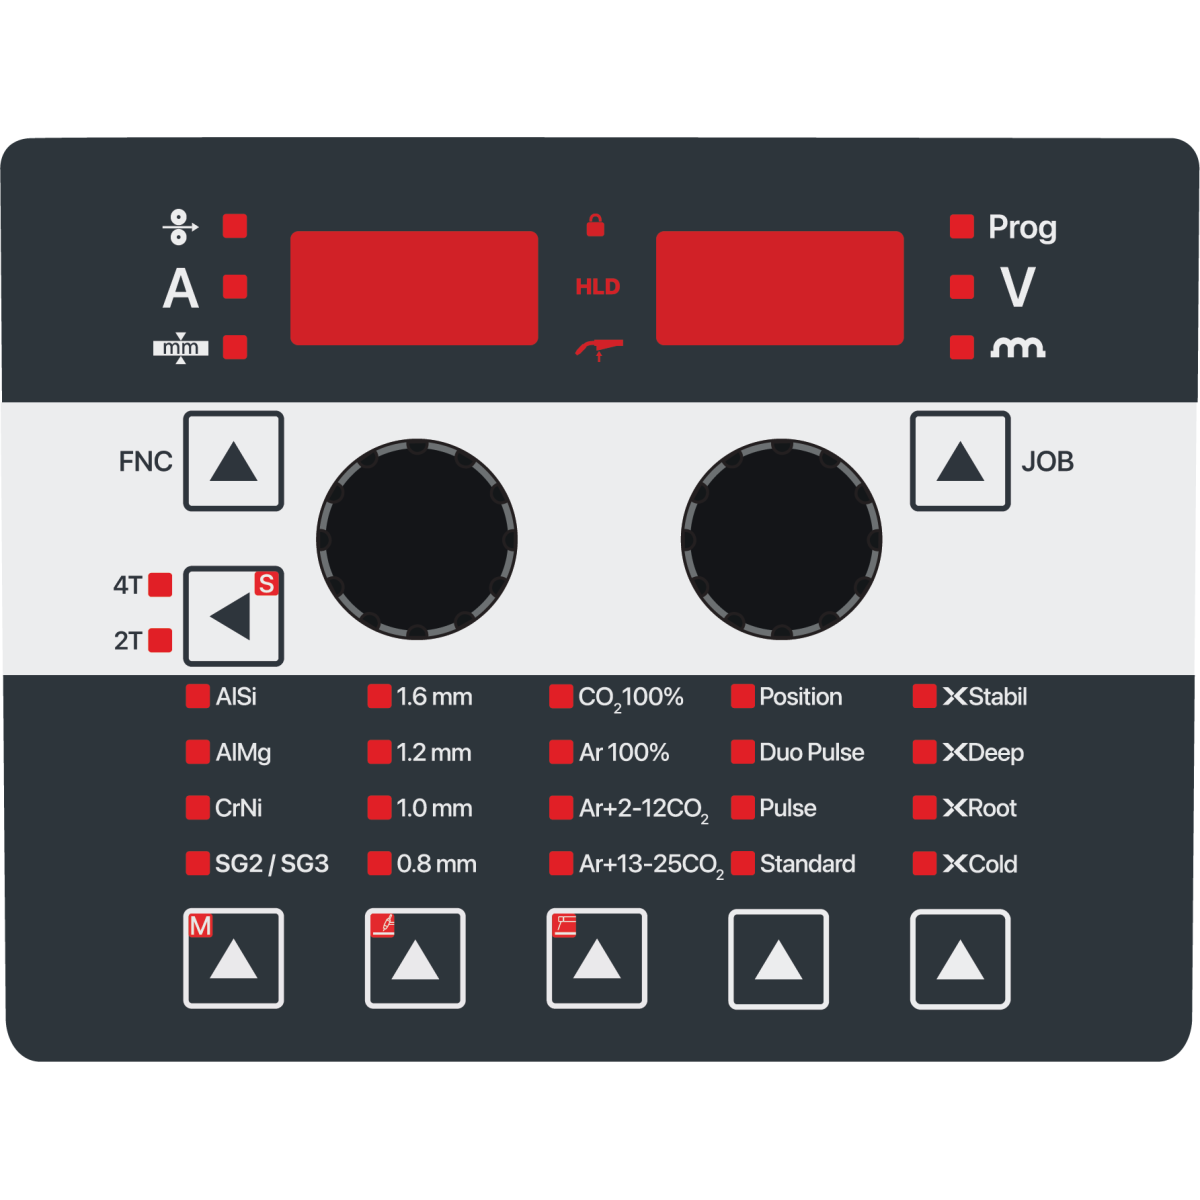
Intuitive design for easy use
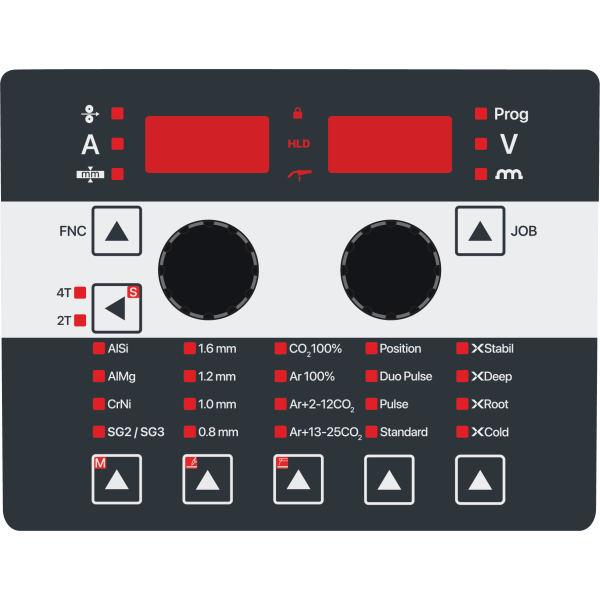
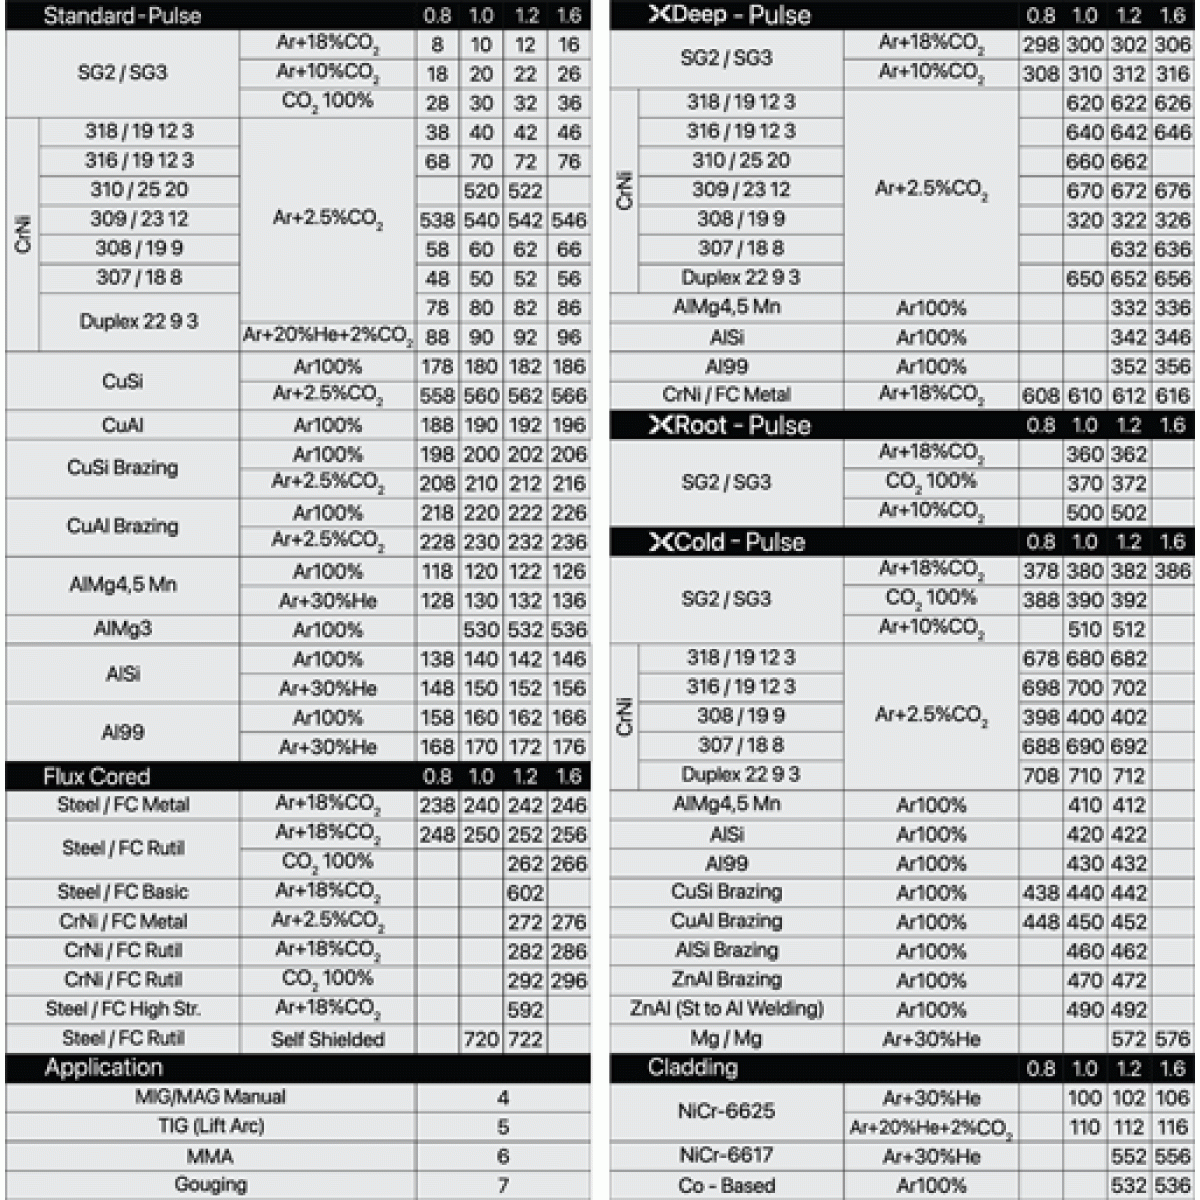
The XM220 C Pulse offers an intuitive interface that highlights the settings users use most frequently. In addition, job and function tables with hundreds of options are available in the background to provide detailed operating options.
Experience 450 welding program
XM220 C Pulse has 450 welding programs that facilitate the welding of steel, stainless steel, aluminum, copper, and zinc alloys, eliminating spatter and the need for post-weld grinding, and it has a memory capacity of 99 programs.
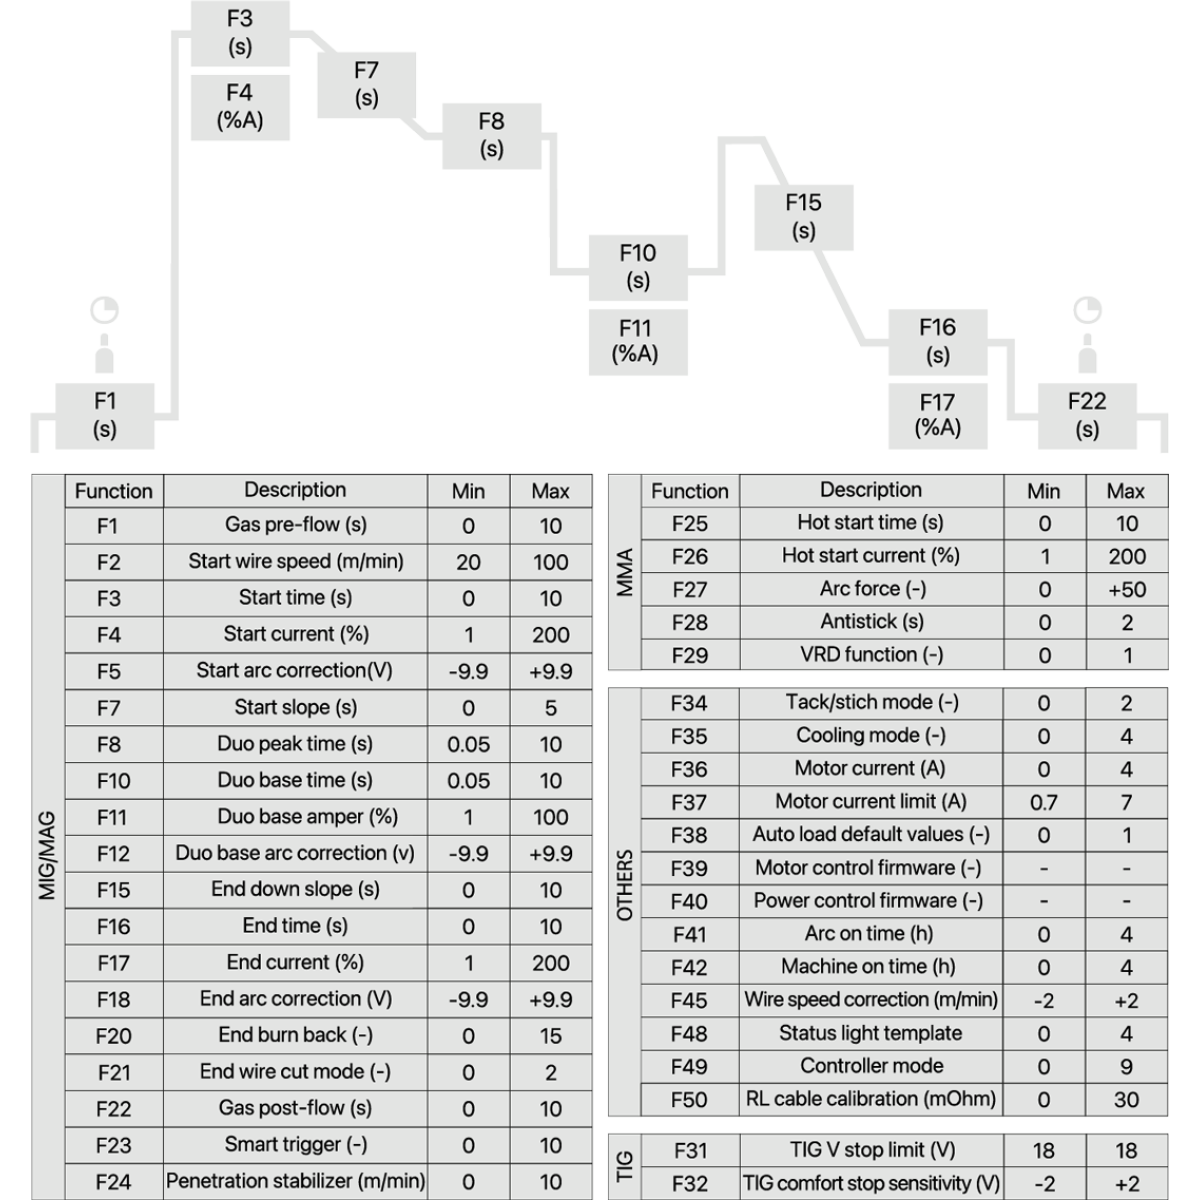
Advanced function table
Function table for MIG/MAG, TIG and MMA welding, allowing advanced settings to be adjusted as needed. Maximizes the welding experience.
High welding speed, low heat input
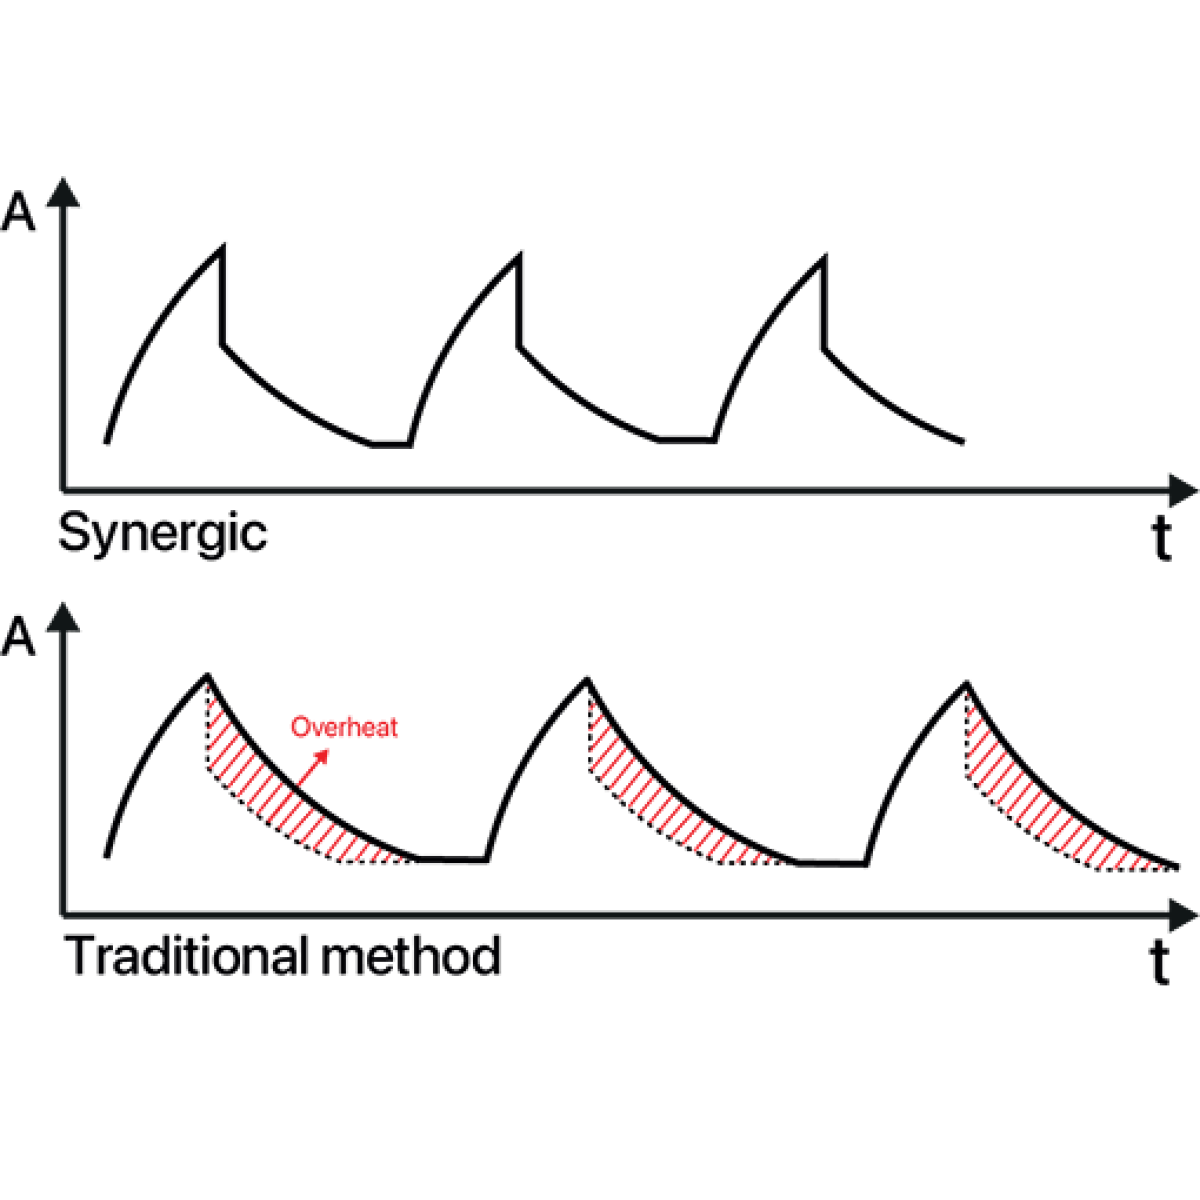
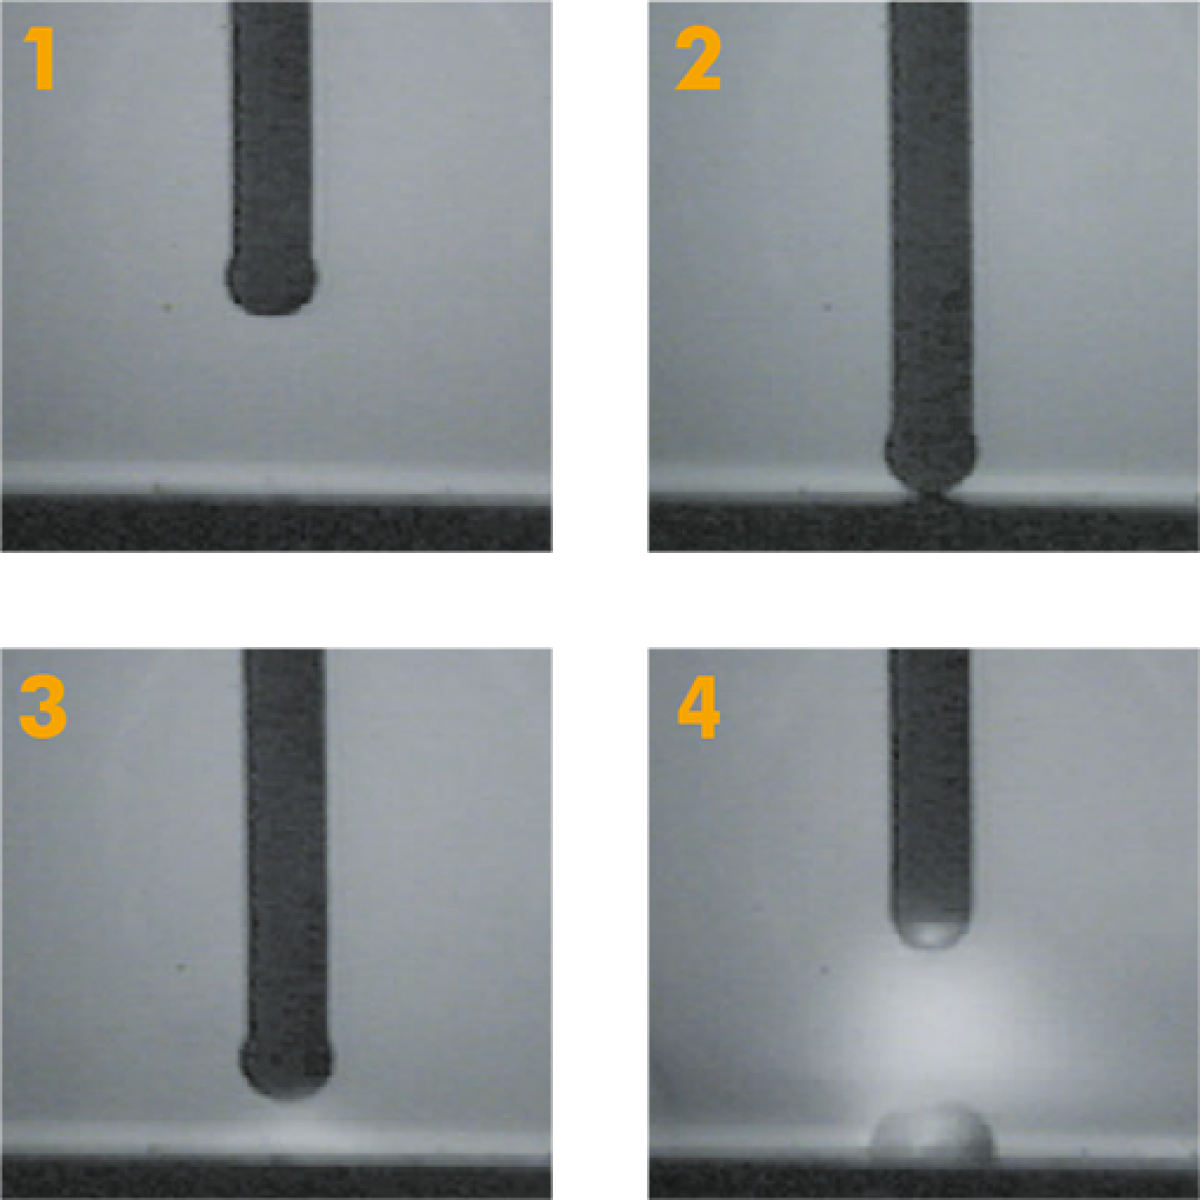
Synergic keeps the voltage constant after droplet transfer by rapidly reducing the welding current vertically to a certain reference level. This increases the welding speed, resulting in low heat input and an intensified arc.
No spatter welding technique
Pulse eliminates post-weld cleaning and spatter in the welding of aluminum, stainless steel and all metal alloys, providing flawless welding performance.
Flawless welding of thin materials
Duo Pulse effectively performs in high and low welding power cycles, providing penetration at high power and cooling the weld pool at low power. These features enable achieving flawless results in thin materials, corner welds, and high precision applications.
Easy control in vertical and overhead welding positions
Position works effectively in both high and low welding power cycles, providing penetration at high power and cooling the weld pool at low power. These features enhance control and confidence when working in vertical and overhead welding positions.
Eliminate high heat input
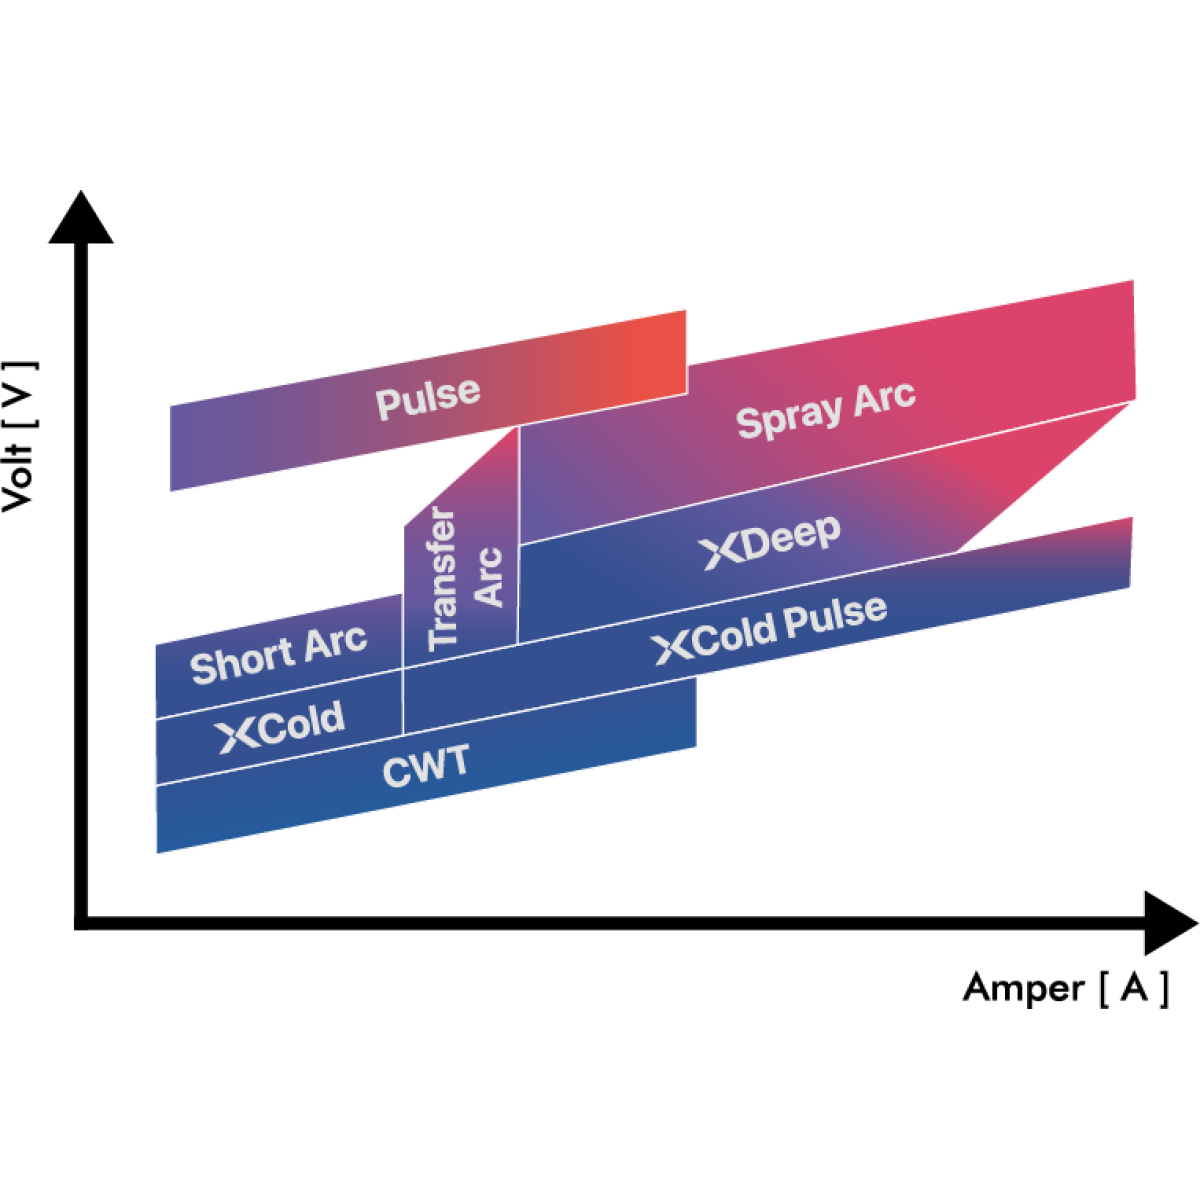
XCold, performing short circuits at a low current level, enables high melting power and quality weld seams with low heat input.
Highly efficient root source
XRoot, performing short circuits at a low current level, provides excellent root penetration with high arc pressure for gap bridging in all positions.
High welding efficiency in thick metals
XDeep operates in the spray arc area. With high-frequency and low-amplitude current pulses, it provides high feed rate and low heat input, especially in steel and stainless steel welding applications in the PA and PB positions. This effectively reduces labor time and welding costs.
100% Penetration
If the free wire length is high (the contact nozzle is too far from the workpiece), the reference current drops and the penetration decreases in order to keep the voltage constant. If the reference current is lower than expected, XStabil increases the wire speed to prevent the reference current from dropping and keep the penetration constant.
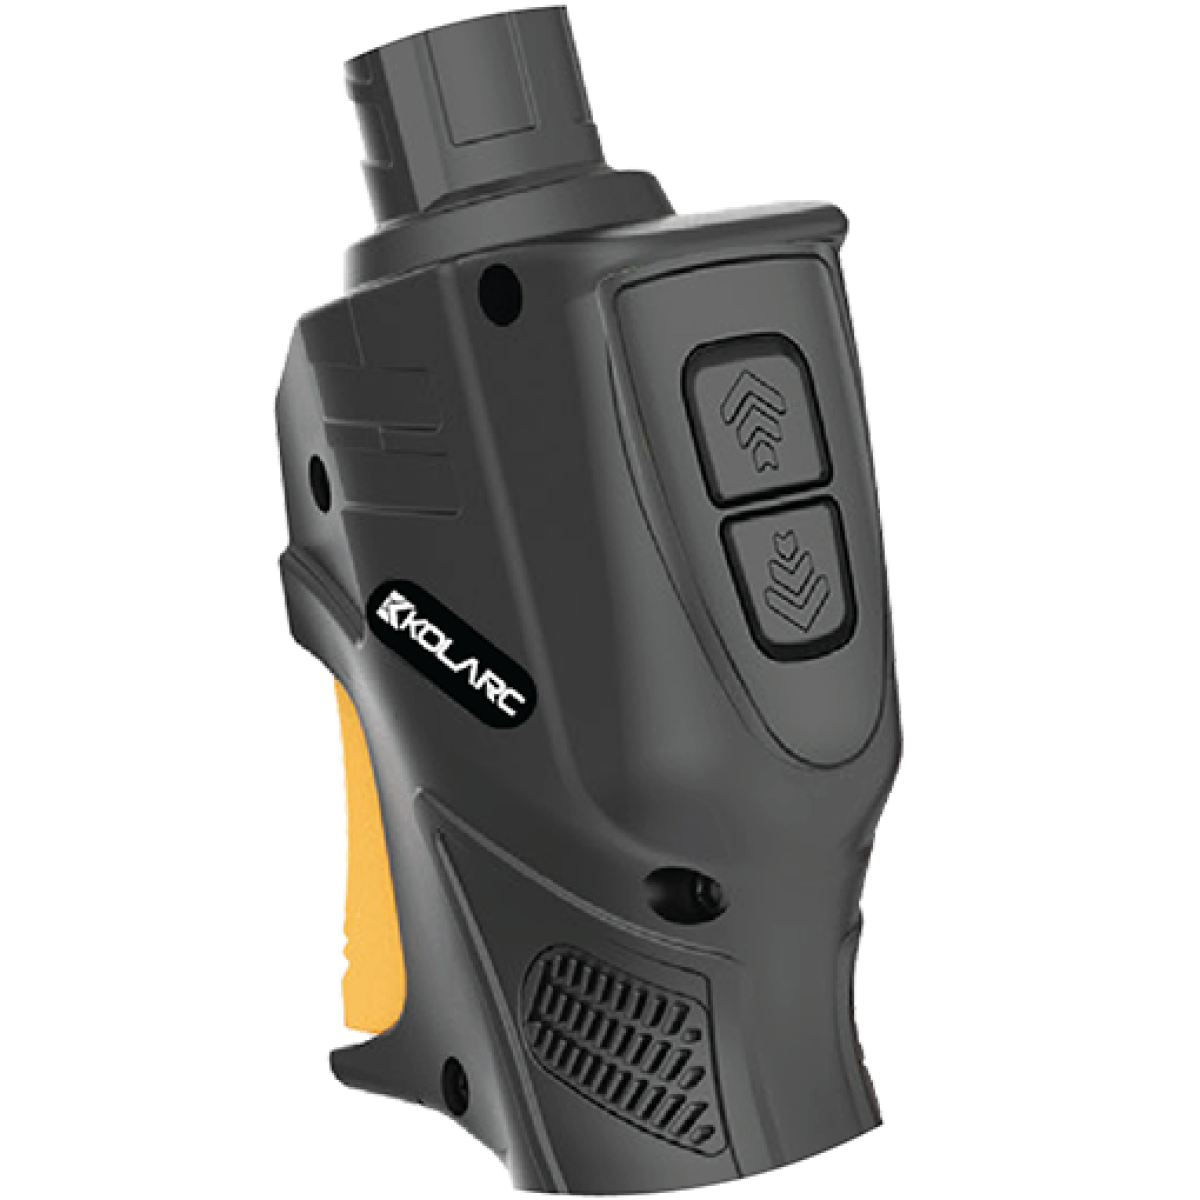
Remote controlled torch
The ability to adjust wire speed, arc height, and program memory before or during welding without accessing the machine’s user interface enhances the comfort and productivity of the welder.
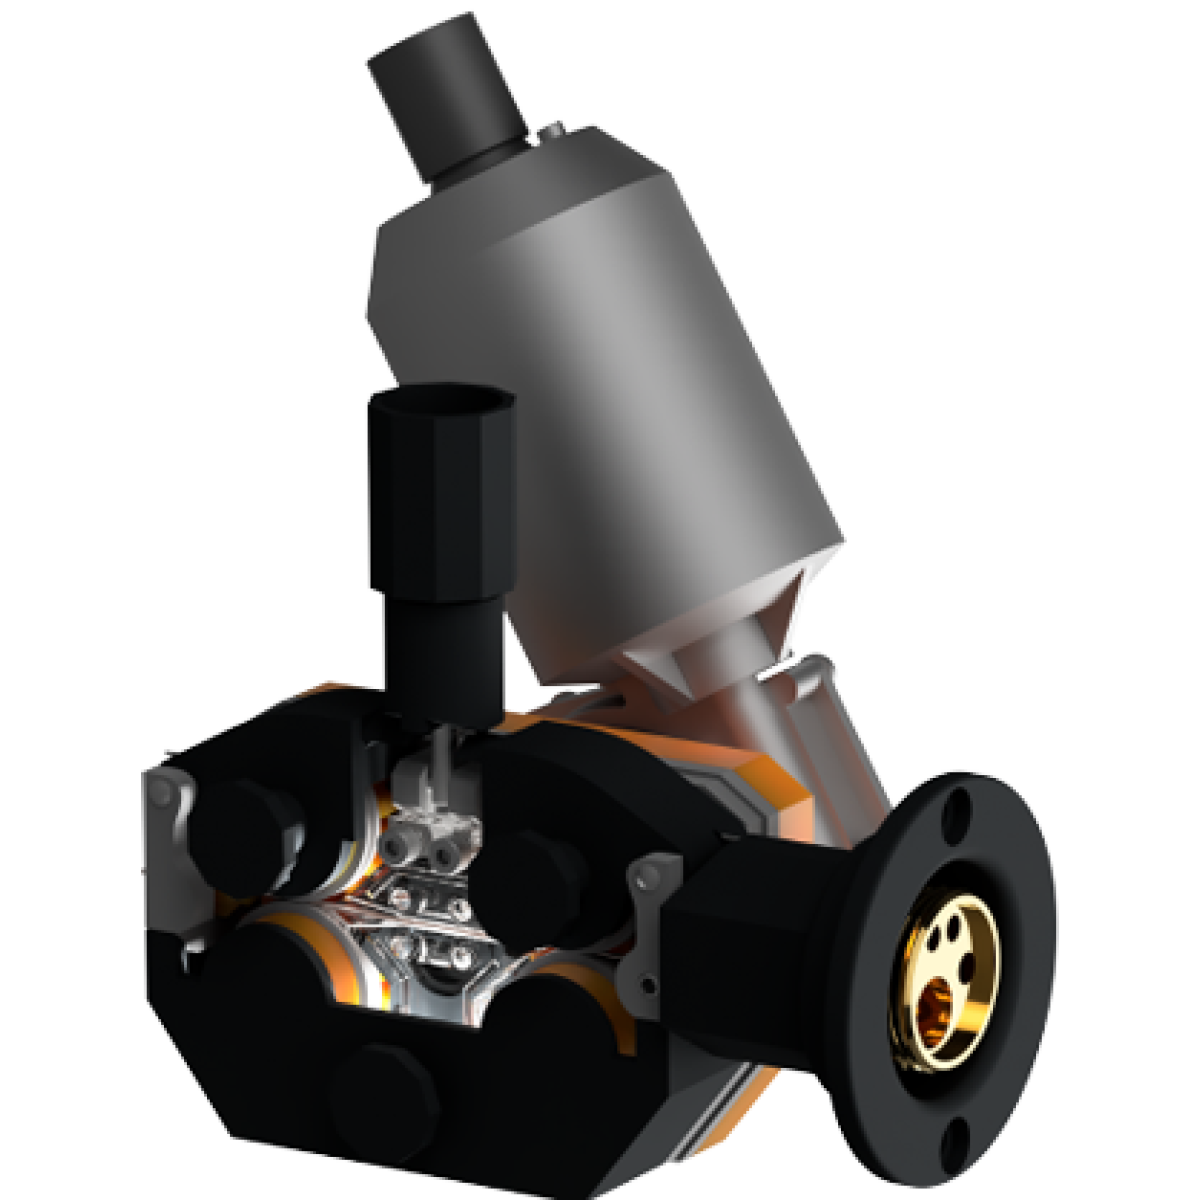
4x4 wire feeder unit
With 4 channels and 4-groove, 32 mm ball-bearing wire feed rollers, a strong grip is provided to the wire without damaging its physical form. This feature enables uninterrupted wire feeding while eliminating wire breakage issues.
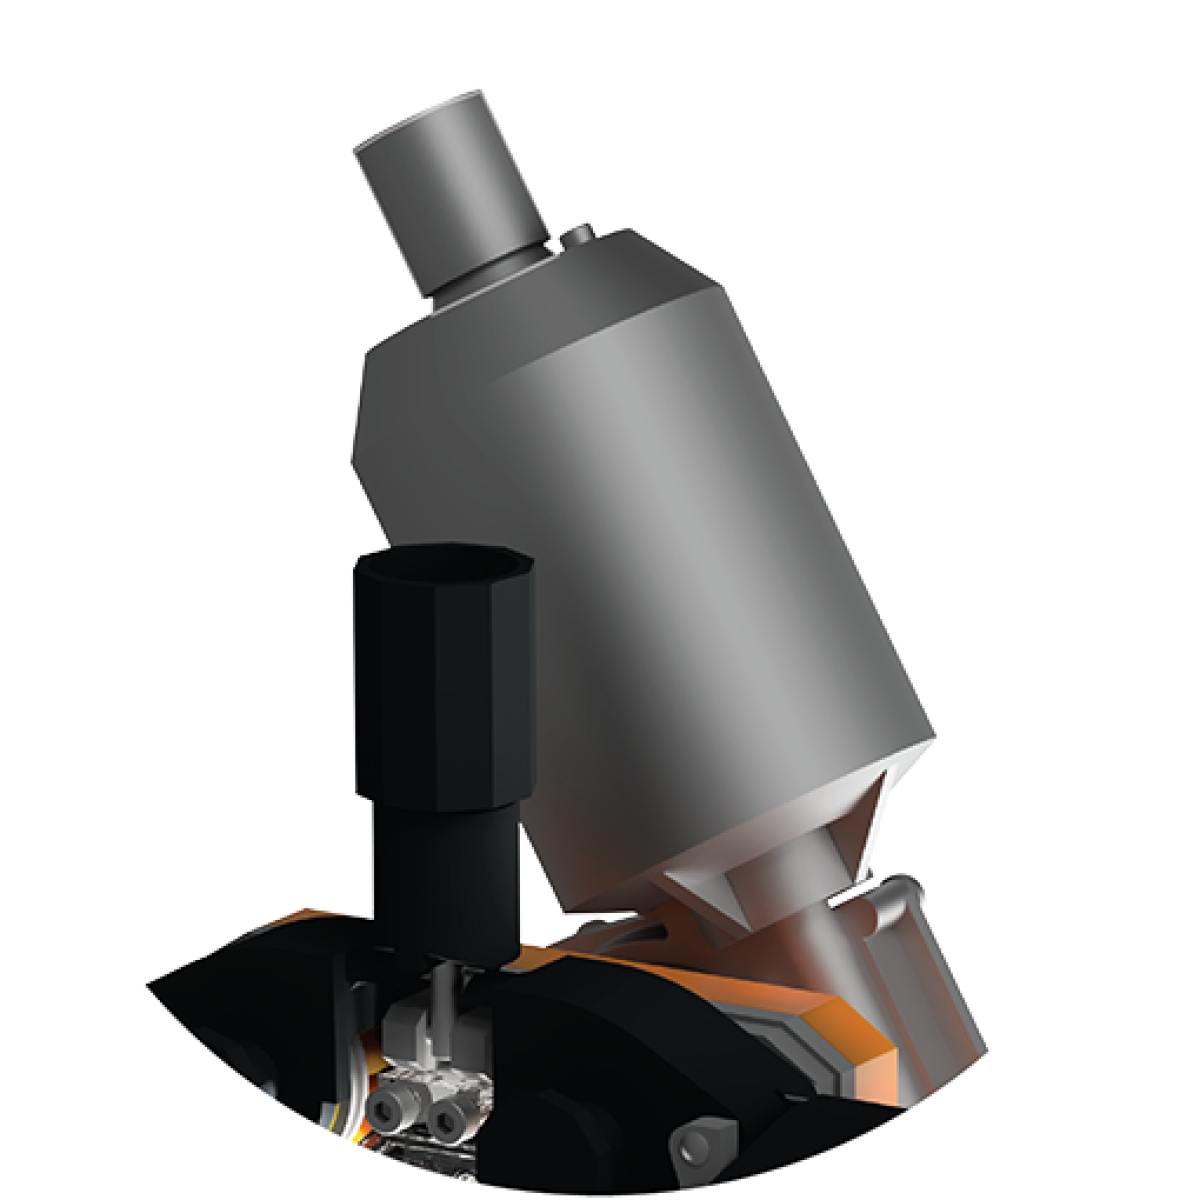
256 PPR optical counter
By controlling the wire speed 50.000 times per second, it ensures that the welding wire reaches the weld pool at a constant rate. This feature minimizes the impact of conditions that negatively affect wire feeding speed on the weld, such as torch bending, contamination in the wire path, and narrowing of the contact tip diameter.
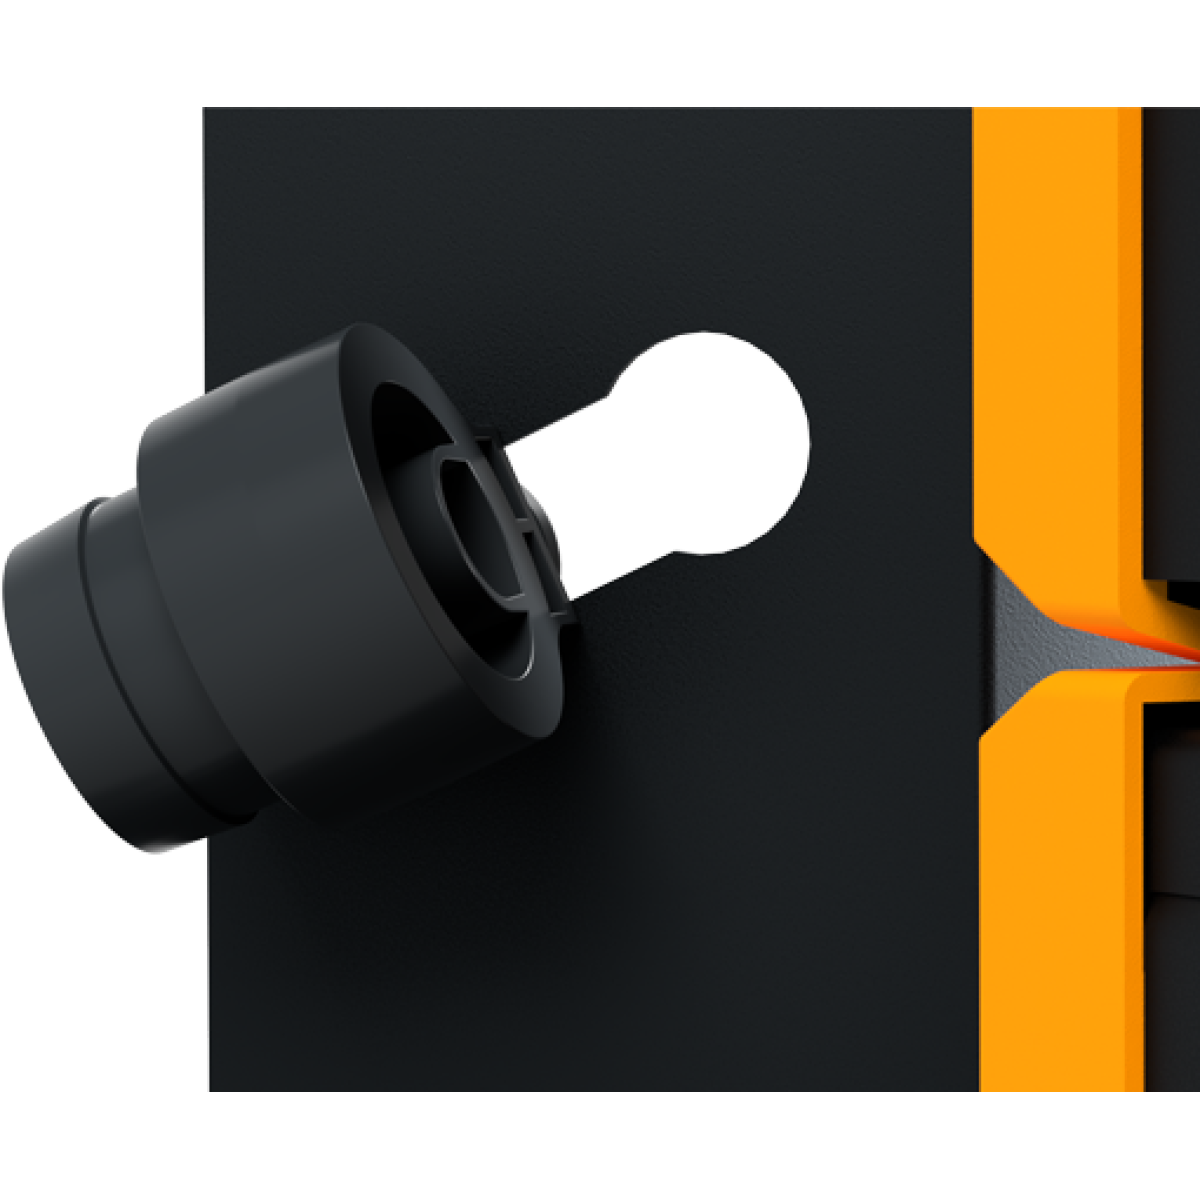
Hose pack support
The easily removable hose support ensures that the power cable, communication cable, gas and water hose components are securely attached to the machine. It also prevents damage to the hose package by preventing the outer cover from peeling off during movement.
Wire forward, wire retract, and gas test
Allows wire and gas adjustments to be made quickly, easily and safely before welding. Prevents gas waste.
Smart cooling
Intelligent cooling fan technology, which is only activated when needed, reduces noise, dust accumulation inside the machine and energy consumption. Increases cooling fan fluid pump life up to 7 times.
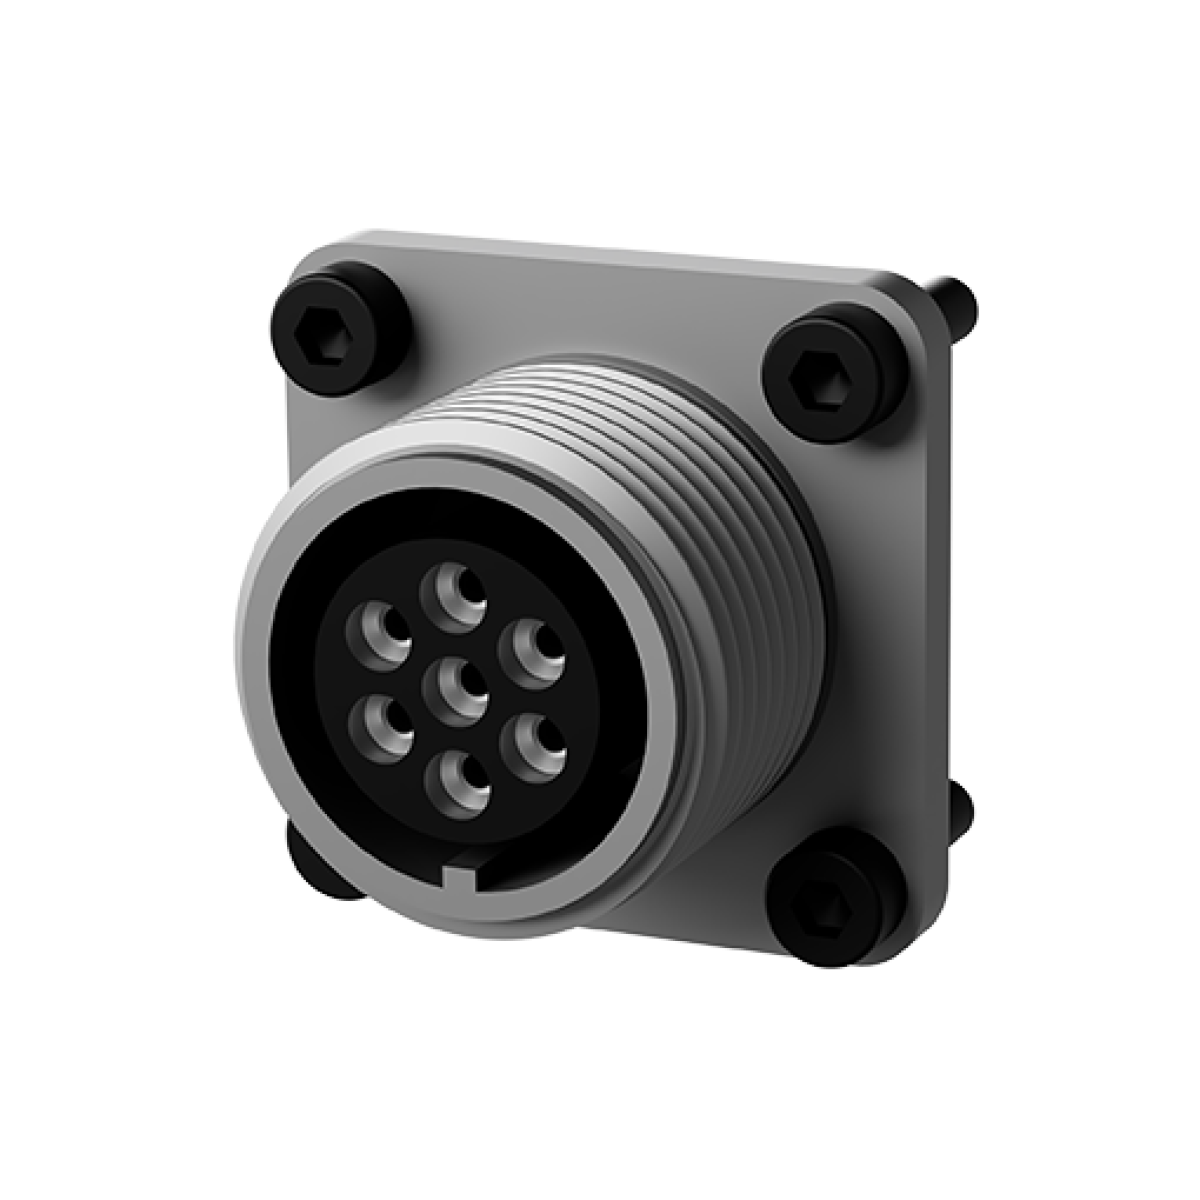
Military standard connector
It offers durability, sealing, protection against electromagnetic interference, high transmission performance and easy removal and installation.
Touch arc ignition
Unique arc starting parameters are applied for each job. The wire makes contact with the workpiece at a lower wire speed. When the arc is initiated, the wire speed automatically increases. This technology reduces contact tip wear, increases productivity, and prevents starting errors in the welding arc.
Adaptive arc control
A dual-core microprocessor with arc control 40,000 times per second regulates the reference current to maintain a constant arc height. This technology improves weld bath control and increases productivity.
Advanced welding processes
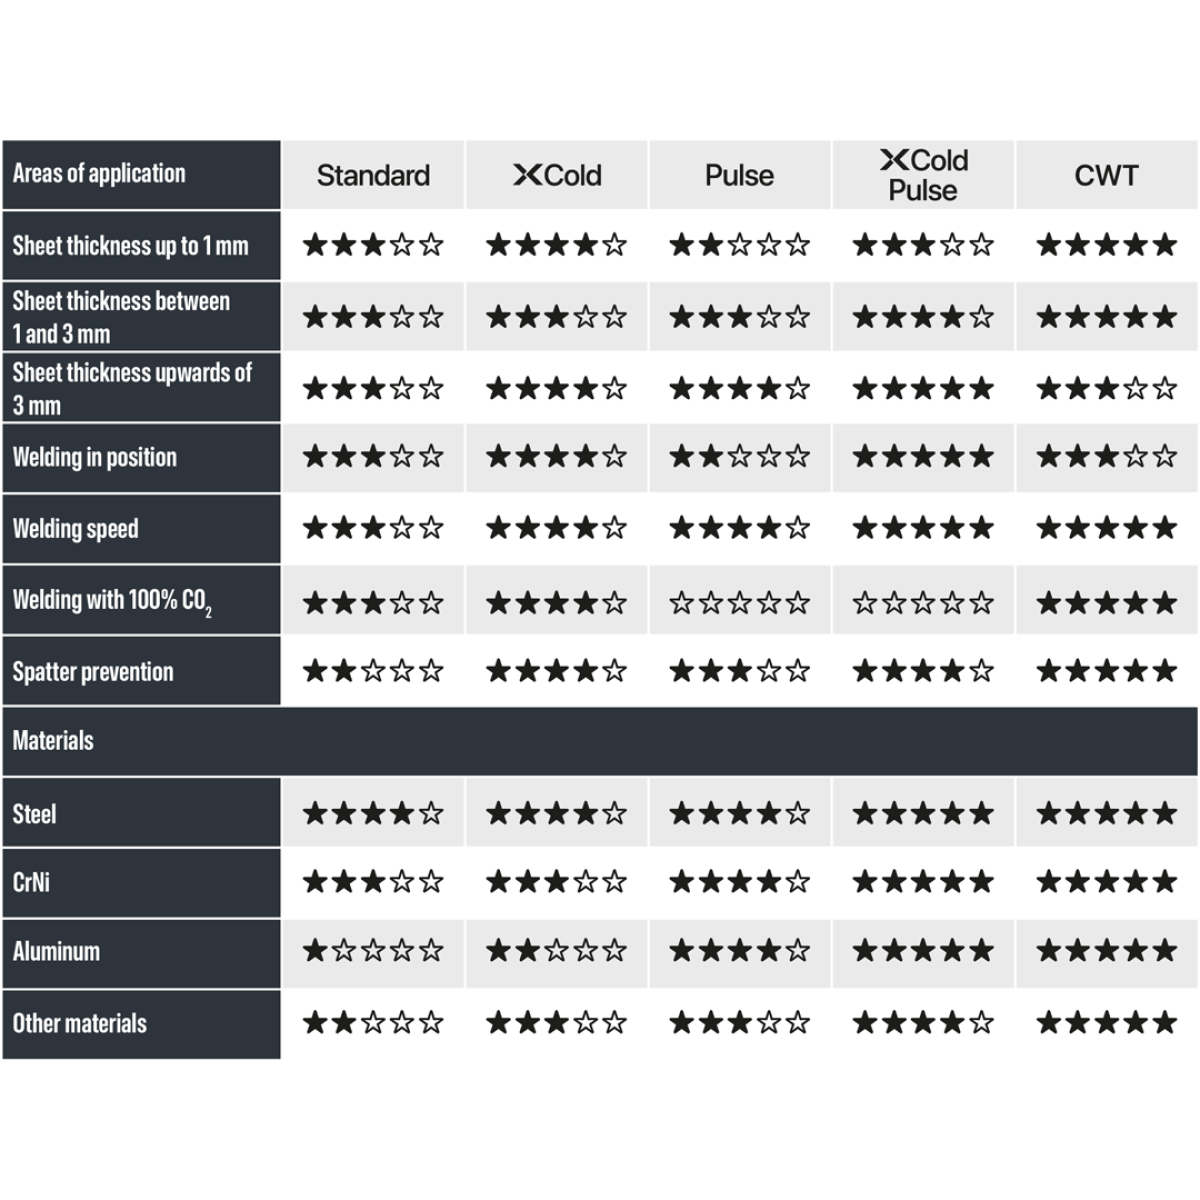
Maximum welding performance with optimized heat input, minimum deformation, high deposition rates and welding speed for aluminum, carbon and stainless steels, and other metal alloys are provided.
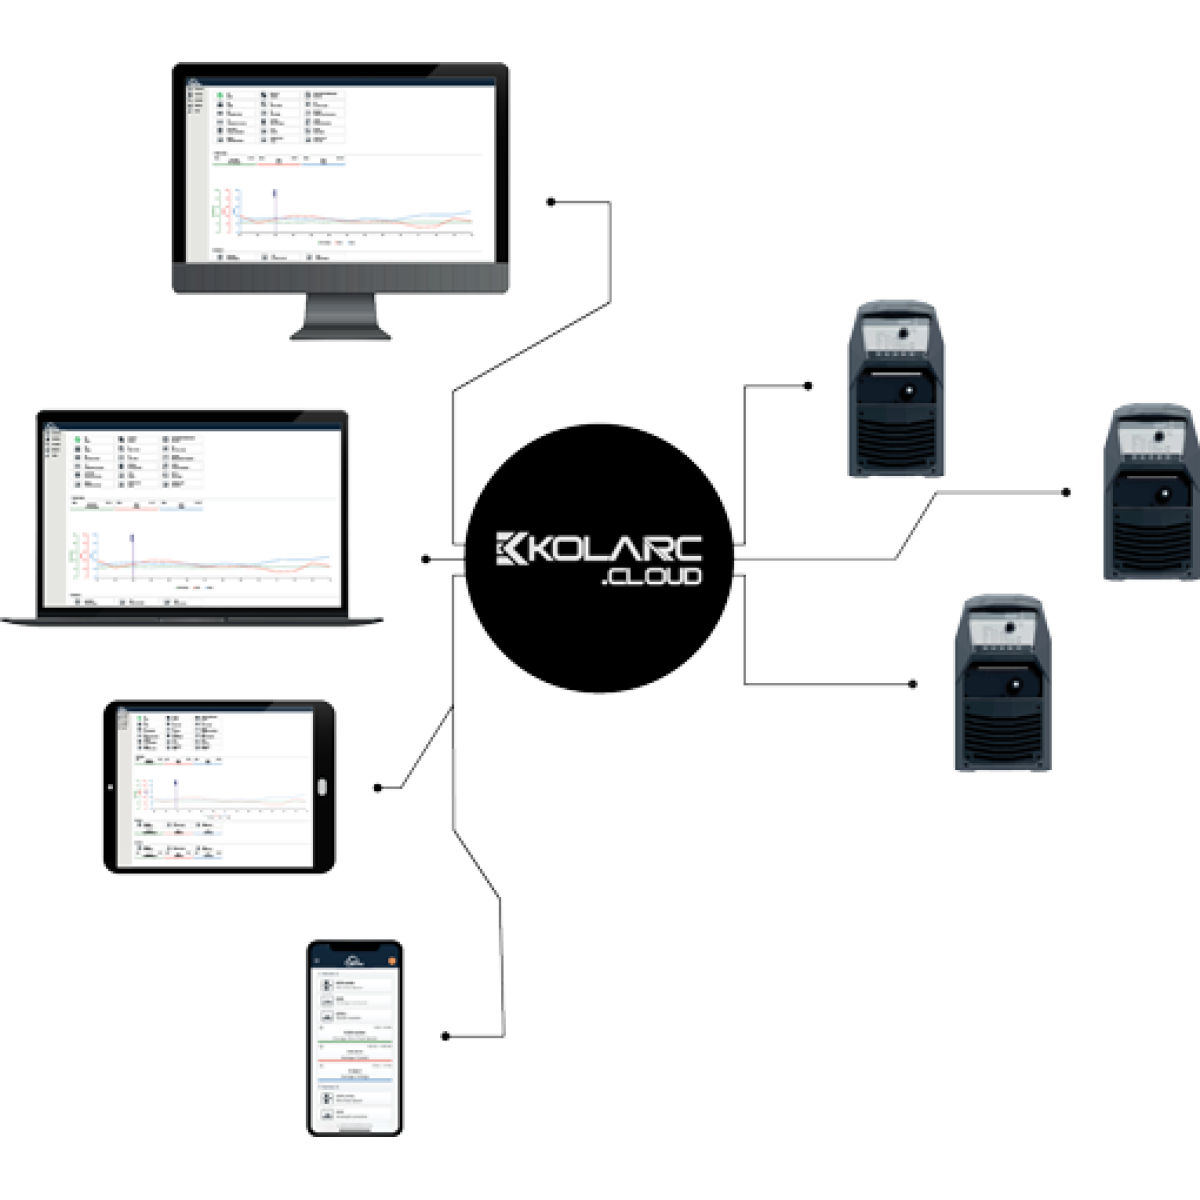
Efficiency, cost optimization, maintenance and quality management are secured with Kolarc.Cloud!
XM220 C
| ERR | 01 | Error-1 Phase error. Occurs when any of the phases does not reach the machine. |
| ERR | 03 | Error-3 IGBT thermal error. Occurs when the IGBTs overheat or when the fan is not operating. (Used in SAW models only.) |
| ERR | 04 | Error-4 Flow sensor error. Triggered when the machine runs out of coolant or when the connectors are not properly inserted. |
| ERR | 05 | Error-5 IGBT thermal error. Occurs when the IGBTs overheat or the fan is not operating. |
| ERR | 06 | Error-6 Diode thermal error. Triggered when the output diode overheats. |
| ERR | 08 | Error-8 Panel board communication error. Occurs when the panel board fails to communicate with the motor board. |
| ERR | 09 | Error-9 Motor board communication error. Occurs when the motor board fails to communicate with the control board. |
| ERR | 10 | Error-10 Con trol board communication error. Triggered when the control board fails to communicate with the panel. |
| ERR | 12 | Error-12 Overcurrent error. Occurs when the machine attempts to draw excessive current or when one of the phases is missing. |
| ERR | 14 | Error-14 Overcurrent protection error. Usually triggered by an IGBT malfunction. |
| ERR | 15 | Error-15 It occurs when there is a problem at +15 or -5 volts. It can also trigger this error if the current sensor is faulty. |
| ERR | 20 | Error-20 Robot board communication error. Occurs when the robot board fails to communicate with the control board. |
| ERR | 30 | Error-30 Motor overcurrent error. Triggered when the motor current exceeds its defined limit. |
| ERR | 40 | Error-40 Memory read/write error. Occurs when the panel fails to read or write data. When this error occurs, the panel automatically resets after 5 seconds and attempts to read/write again. |
- Input Voltage: 230 V
- Mains Voltage Tolerance: -10 % / +15 %
- Minimum Welding Current: 10 A
- Maximum Welding Current: 220 A
- Duty Cycle, 40°C: MIG 220A 30%, TIG 220A 30%, MMA 220A 30% | MIG 120A 100%, TIG 120A 100%, MMA 120A 100%
- Open – Circuit Voltage: 58 V – 75 V
- Factory Delivered Roller: 0.8 + 1.0 mm / Steel
- Weight: Air-Cooled | 34 kg
Technical documentation: Manuals or product documents are available for this model.
Produse asemănătoare