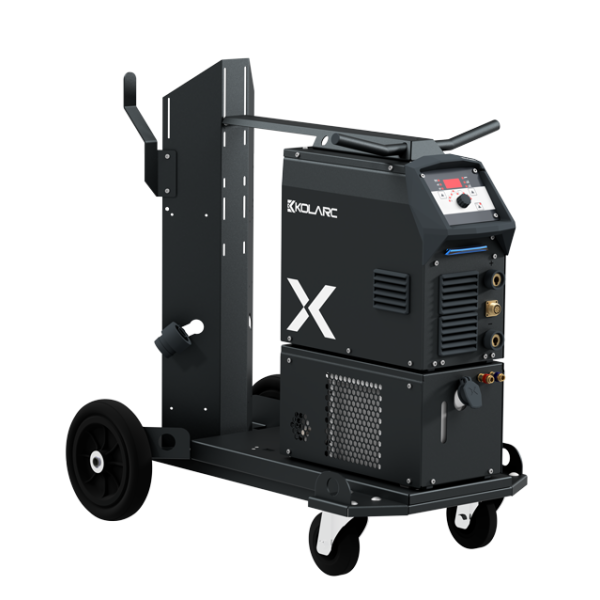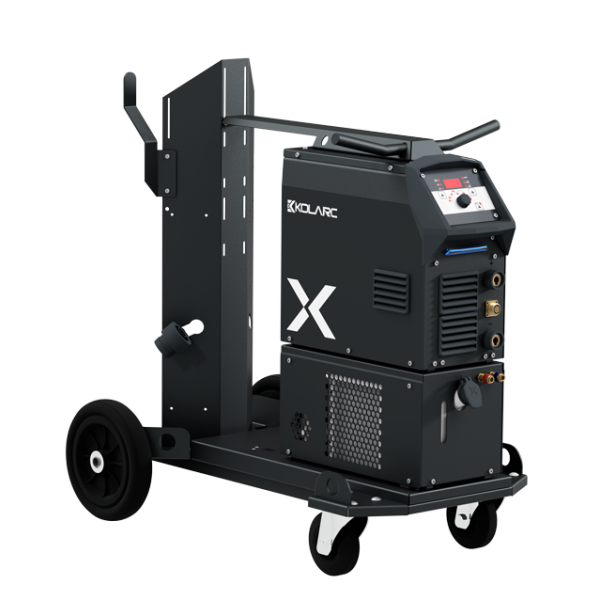
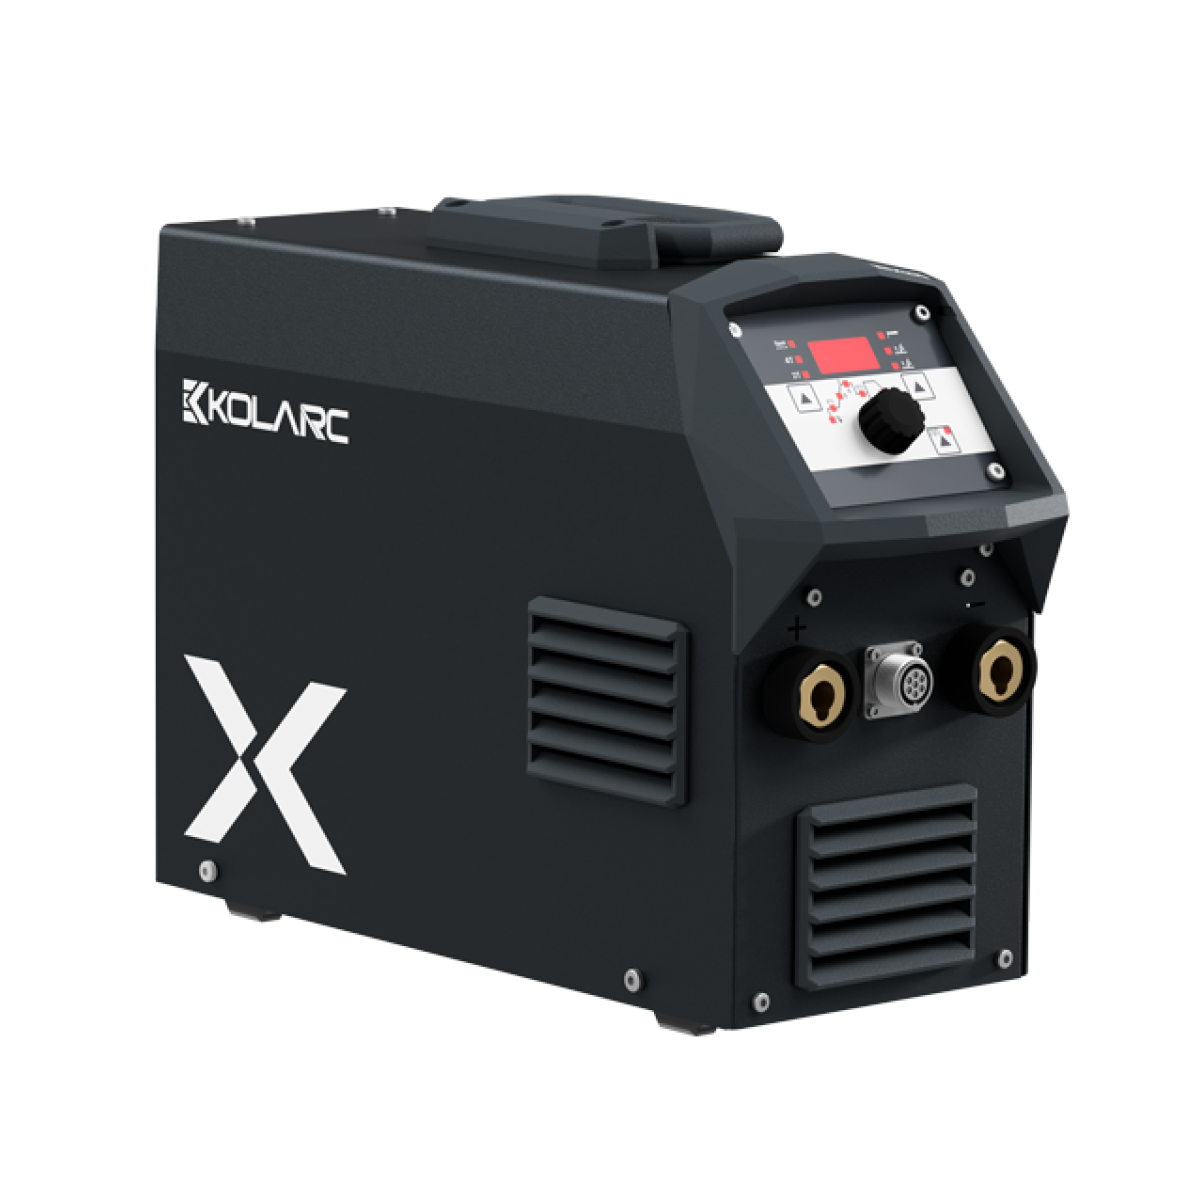
TX400
Model
2Nu am găsit niciun model.
Descriere
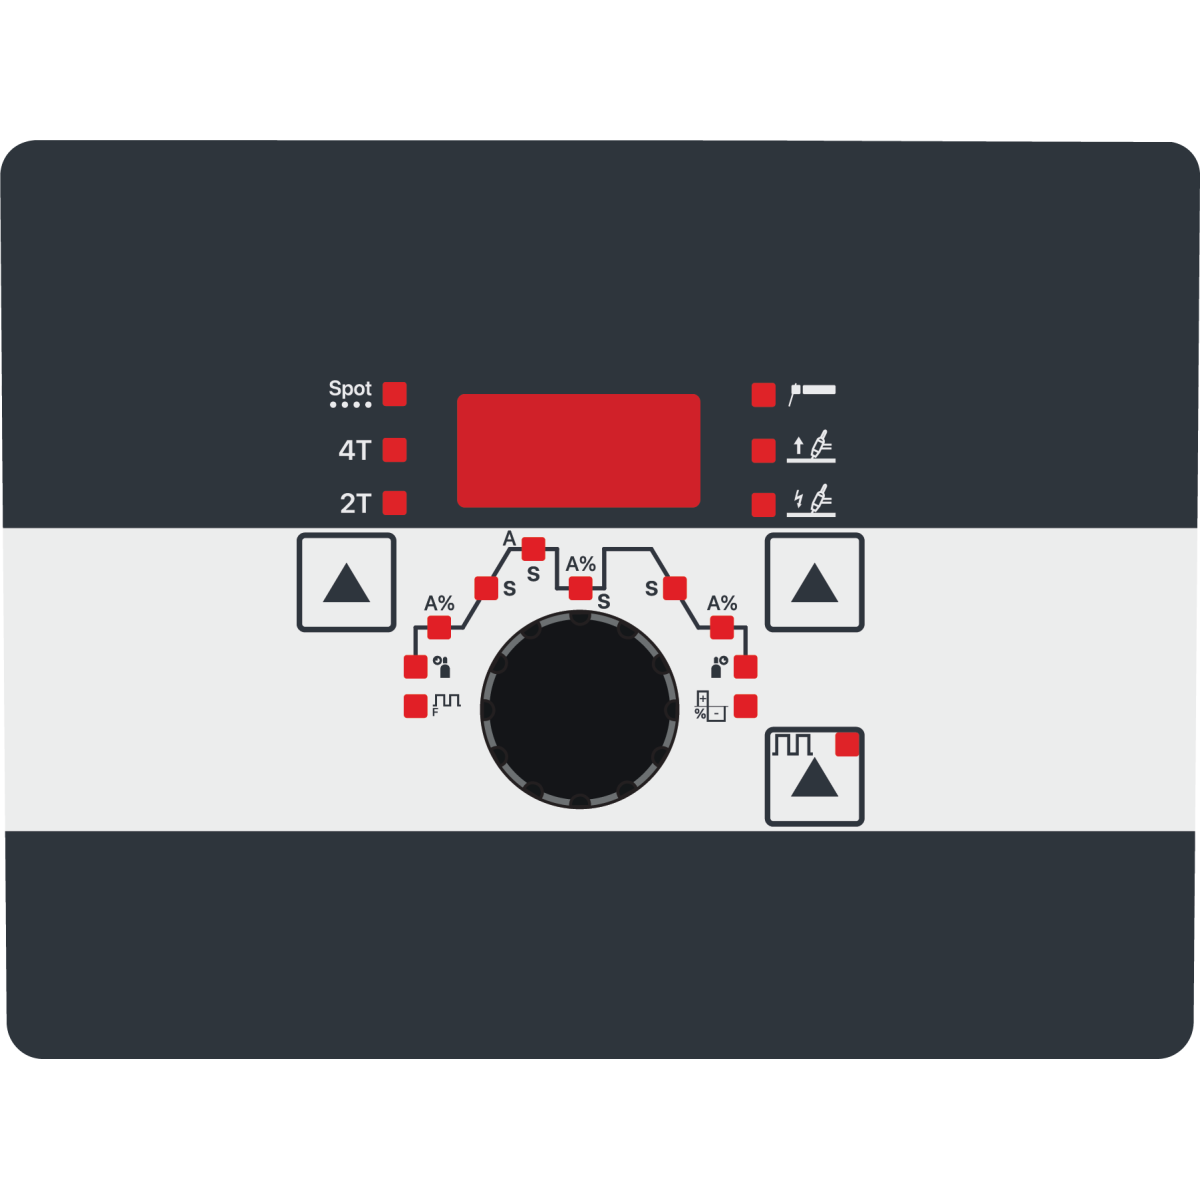
Intuitive design for easy operation
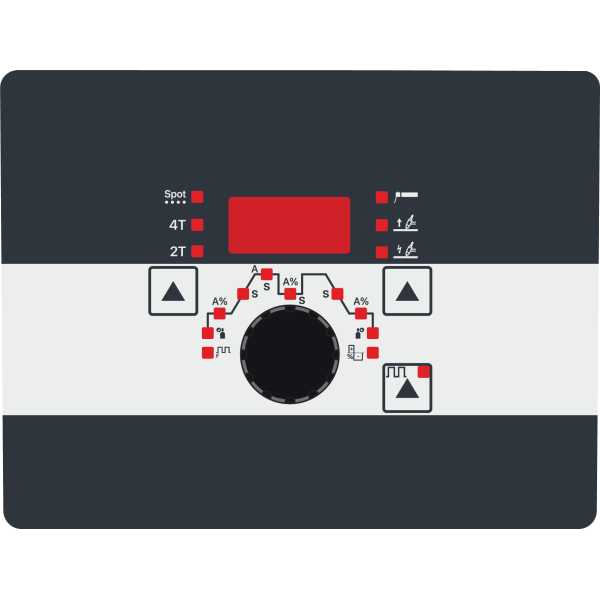
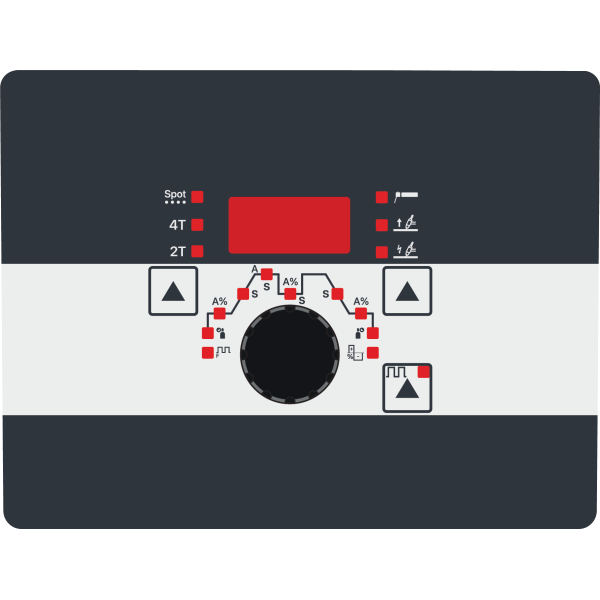
With its customizable feature, you can directly select your source processes by adding 99 programs to your favorite processes. The easy-to-read, intuitive user interface saves you time.
Hot Start
It facilitates the holding of the coated electrode at the beginning of welding, preventing it from sticking.
High frequency ignition
HF high frequency ignition overcomes the air gap between the electrode and the workpiece and prevents direct contact, thus avoiding the formation of tungsten residues after welding.
Lift TIG
Without high frequency and high voltage, it enables arc initiation without adhesion by touching the electrode to the workpiece.
2T/4T
Manual and automatic triggering improves the welder’s control capability and working ergonomics.
Aesthetic spot welds
The spot function is the application of a predetermined current intensity and duration to the weld metal at a fixed electrode distance, especially with the touch and breakaway motion. In this way, the current intensity, duration and arc height are adjusted by the machine to achieve 100% repeatable spot welding results.
sPulse
sPulse provides precise handling, low heat input, high melting strength and quality weld seams thanks to the independent adjustment of the duration of the pulse top current and bottom current.
FPulse
FPulse provides easy use, low heat input, high melting power, and quality weld seams thanks to the ability to adjust the pulse peak current and base current in a frequency-dependent 50/50 ratio.
APulse
APulse provides fast handling, low heat input, high melting power and quality weld seams thanks to synergic adjustment of the pulse frequency depending on the main current.
Highly efficient root source
CEL enables continuous arc welding on cellulosic electrodes, resulting in weld seams with a flawless appearance. It offers adapted welding characteristics for more efficient use in position welding.
Consistent welding penetration and secure root joint
It enables the electrode to melt without sticking at low current levels according to the electrode diameter. It facilitates welding by reducing heat input in position welding.
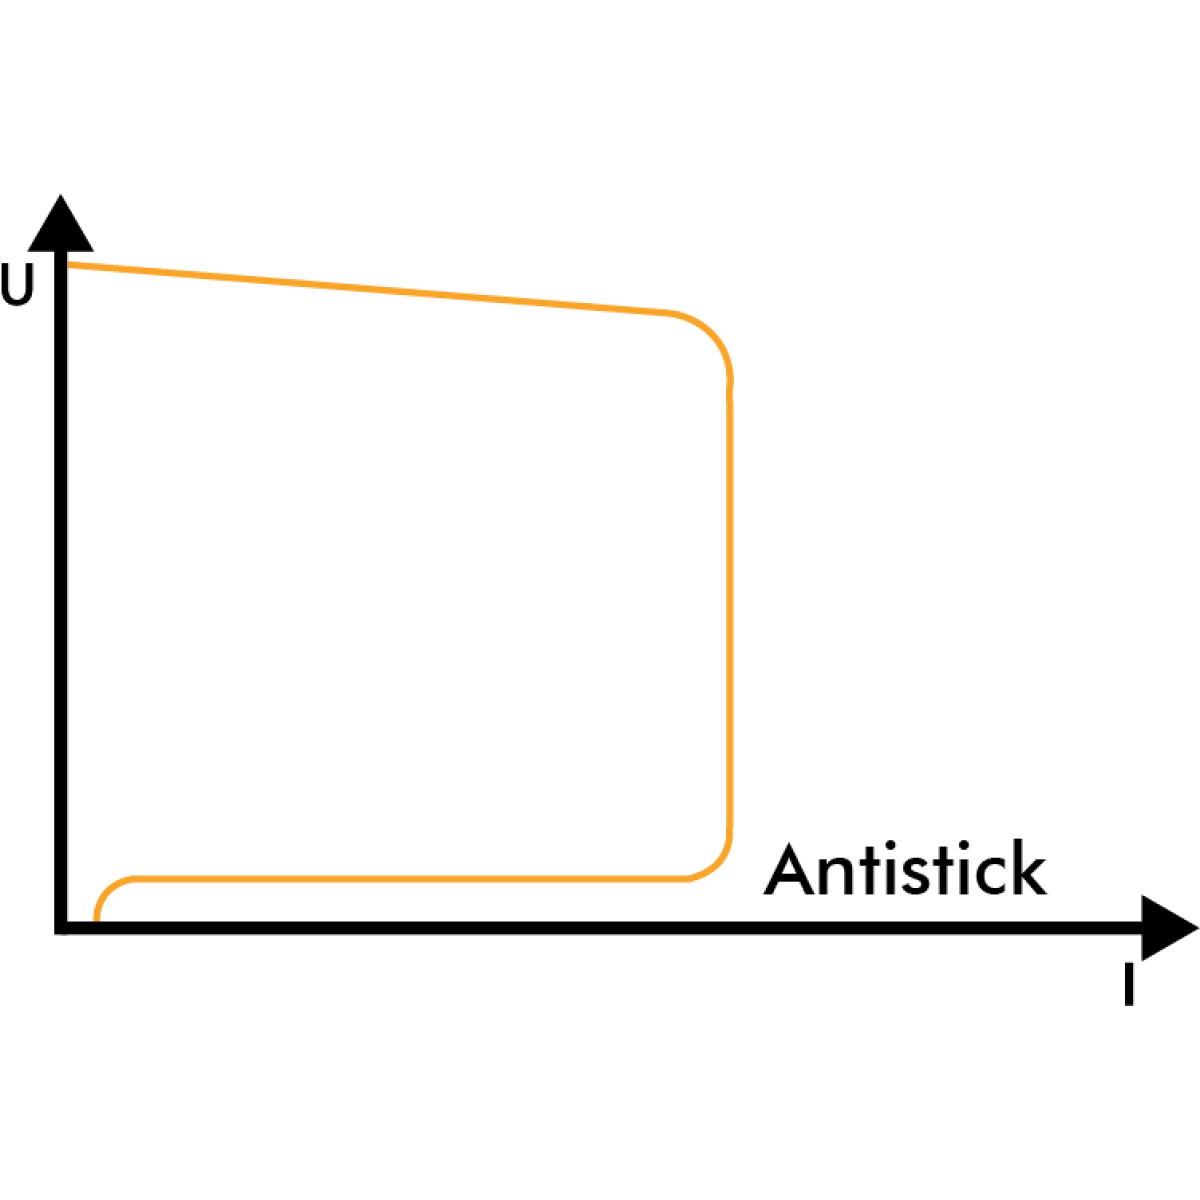
Smart power supply
If the electrode sticks to the workpiece, it provides easy separation and prevents damage to the electrode.
TX400
| ERR | 01 | Error-1 Phase error. Occurs when any of the phases does not reach the machine. |
| ERR | 03 | Error-3 IGBT thermal error. Occurs when the IGBTs overheat or when the fan is not operating. (Used in SAW models only.) |
| ERR | 04 | Error-4 Flow sensor error. Triggered when the machine runs out of coolant or when the connectors are not properly inserted. |
| ERR | 05 | Error-5 IGBT thermal error. Occurs when the IGBTs overheat or the fan is not operating. |
| ERR | 06 | Error-6 Diode thermal error. Triggered when the output diode overheats. |
| ERR | 08 | Error-8 Panel board communication error. Occurs when the panel board fails to communicate with the motor board. |
| ERR | 09 | Error-9 Motor board communication error. Occurs when the motor board fails to communicate with the control board. |
| ERR | 10 | Error-10 Con trol board communication error. Triggered when the control board fails to communicate with the panel. |
| ERR | 12 | Error-12 Overcurrent error. Occurs when the machine attempts to draw excessive current or when one of the phases is missing. |
| ERR | 14 | Error-14 Overcurrent protection error. Usually triggered by an IGBT malfunction. |
| ERR | 15 | Error-15 It occurs when there is a problem at +15 or -5 volts. It can also trigger this error if the current sensor is faulty. |
| ERR | 20 | Error-20 Robot board communication error. Occurs when the robot board fails to communicate with the control board. |
| ERR | 30 | Error-30 Motor overcurrent error. Triggered when the motor current exceeds its defined limit. |
| ERR | 40 | Error-40 Memory read/write error. Occurs when the panel fails to read or write data. When this error occurs, the panel automatically resets after 5 seconds and attempts to read/write again. |
- Input Voltage: 400 V
- Mains Voltage Tolerance: -10 /+15 %
- Minimum Welding Current: 10 A
- Maximum Welding Current: 400 A
- Duty Cycle, 40°C: MIG 400A 40%, TIG 360A 60%, MMA 320A 100%
- Open – Circuit Voltage: 63 V – 82 V
- Factory Delivered Roller: 0.8 + 1.0 mm / Steel
- Weight: Liquid Cooling, W | 94 kg